Variant Sets
Long Name Case Study
How to accommodate extreme character lengths inside fixed die-cut geometries without breaking visual weight, optical hierarchy, or margin integrity across your print series.
How to accommodate extreme character lengths inside fixed die-cut geometries without breaking visual weight, optical hierarchy, or margin integrity across your print series.
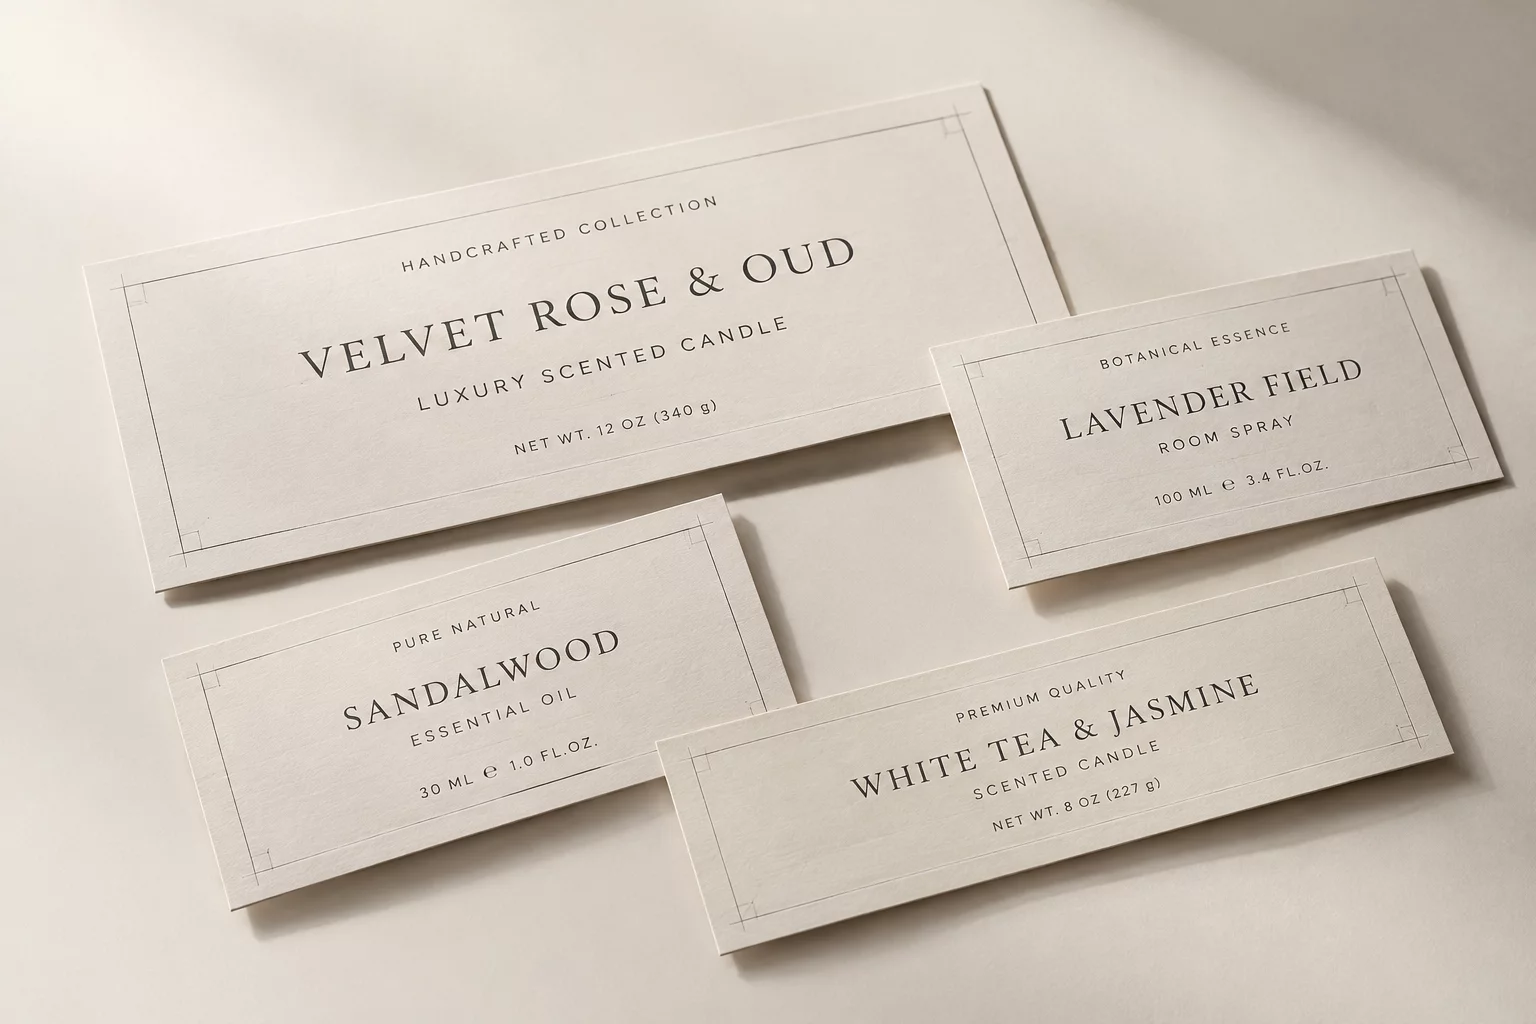
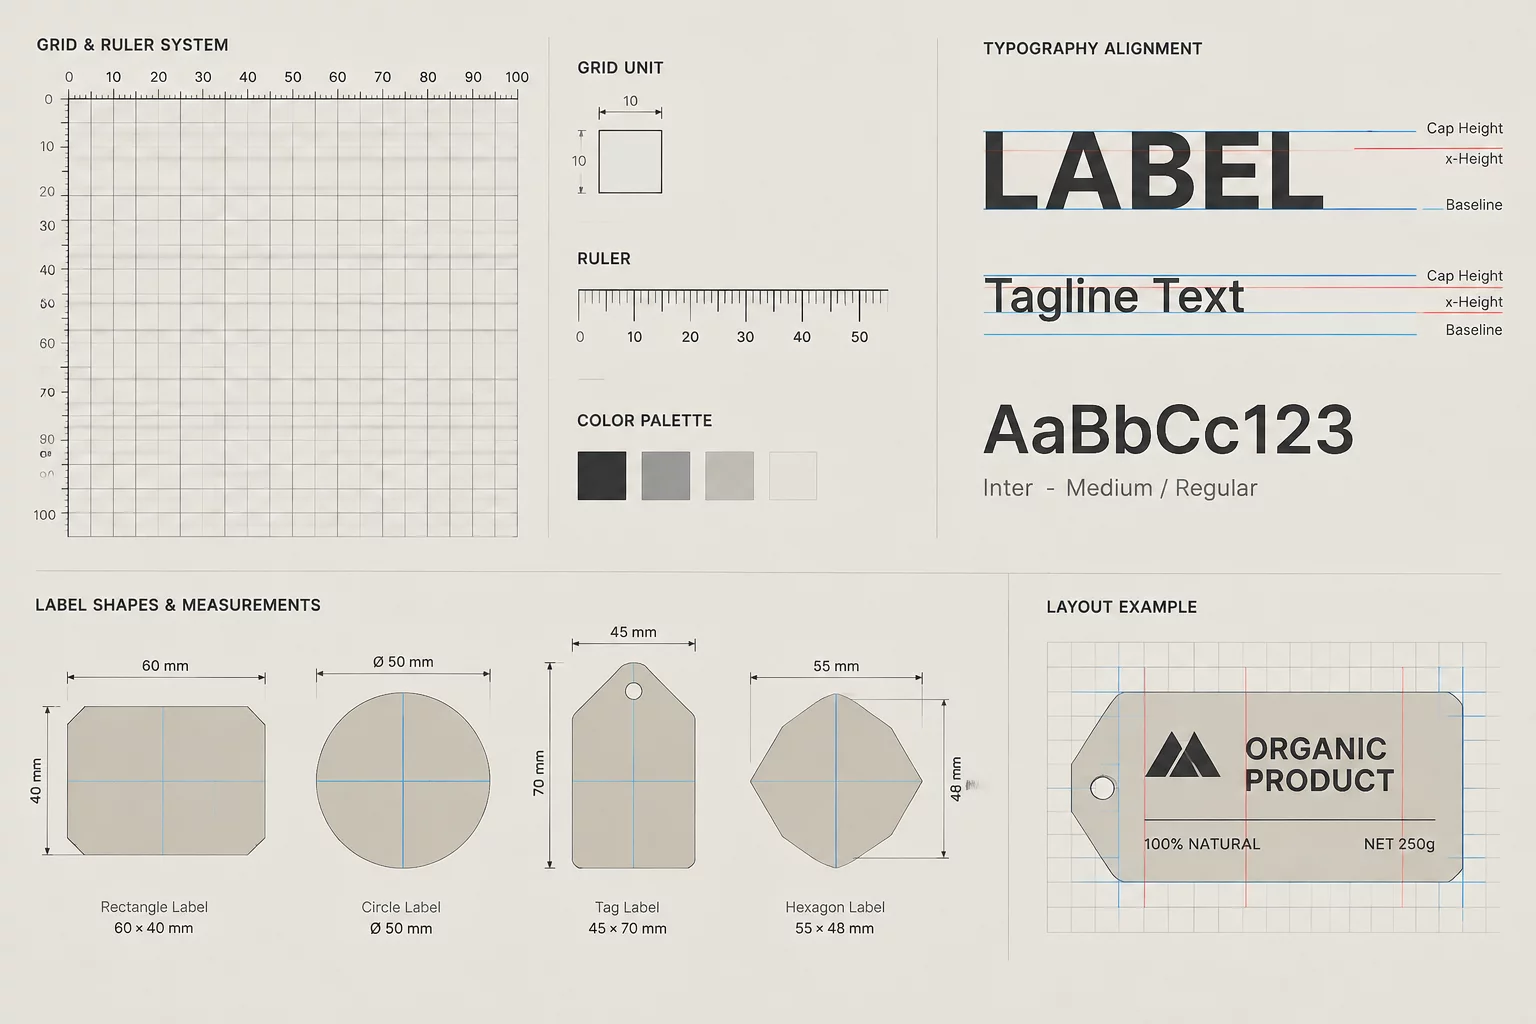
Custom label runs frequently encounter extreme disparity in text string lengths. A short moniker such as "Mia" sits effortlessly with generous breathing room, but compound names like "Christopher-James" or "Alexandrina" instantly collide with inner margins and bleed zones.
Most novice designers respond by arbitrarily shrinking the font size until the entire text fits between the border lines. That approach quickly destroys production consistency. When an eleven-point condensed name sits directly beside a twenty-four-point regular name on the same cutting sheet, the printed collection ceases to look like a curated series. Stroke thicknesses thin out noticeably, delicate counters plug up under toner saturation, and the overall optical balance of the batch collapses.
Rather than jumping straight to radical font point reductions, production designers must enforce an orderly four-tier hierarchy. Each tier tests a controlled visual compensation before altering the core typographic footprint.
Series cohesion does not demand identical point sizes. It demands uniform optical gravity, consistent stroke weight perception, and protected negative space along every die-cut boundary.
First, reduce letter spacing gradually down to a strict floor of minus eighteen units in Silhouette Studio. If the outer glyphs still infringe upon the 3.2 mm safety clearance boundary, switch to the official semi-condensed cut of the font family. When extreme cases like hyphenated surnames require even more horizontal clearance, split the string into a structured two-line stack with proportional leading pegged at ninety percent of cap-height.
Inside Silhouette Studio, activate the smart alignment guides and lock the outer cut boundary onto a dedicated registration layer. Place the master layout bounding box in the center, and define an offset internal perimeter representing your hard boundary buffer. Any variable name that breaches this line triggers the condensation script or the two-line stack rule automatically.
Always output a single drafting proof on 80 lb text weight stock before loading premium vinyl or matte sticker material into your digital cutter. Place the printed proof under neutral gallery lighting alongside short-name samples. When viewed from arms length, both long-name and short-name specimens should project equal dark-to-light ink density across their shared perimeter shapes.
Receive our calibrated margin reference tables, tracking thresholds, and kerning limit cards for Silhouette Studio production sheets.